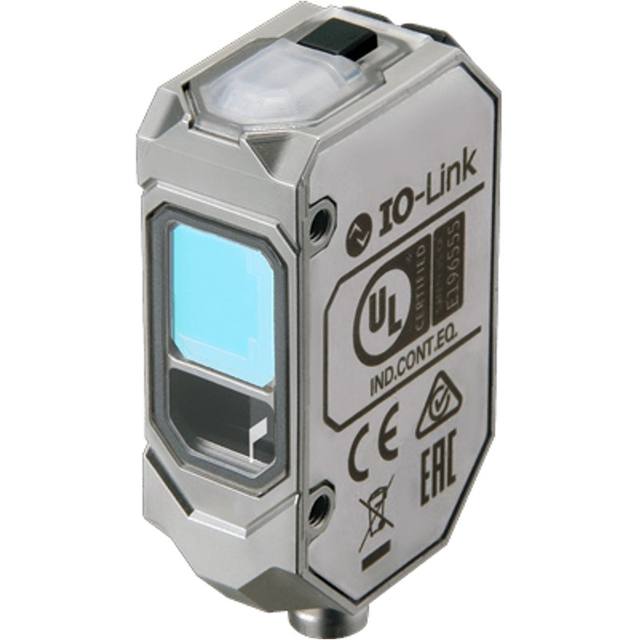
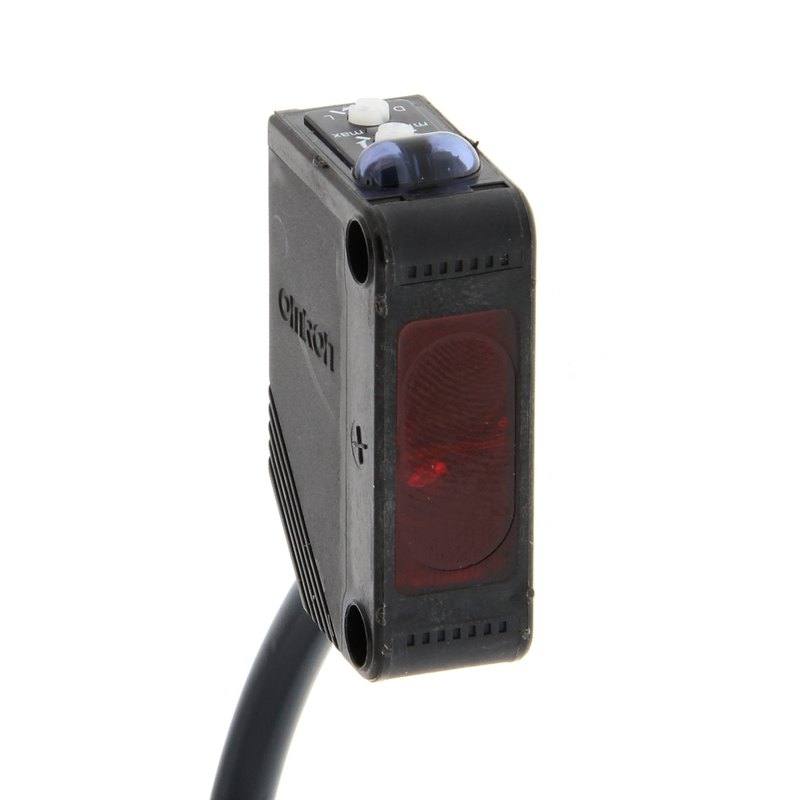
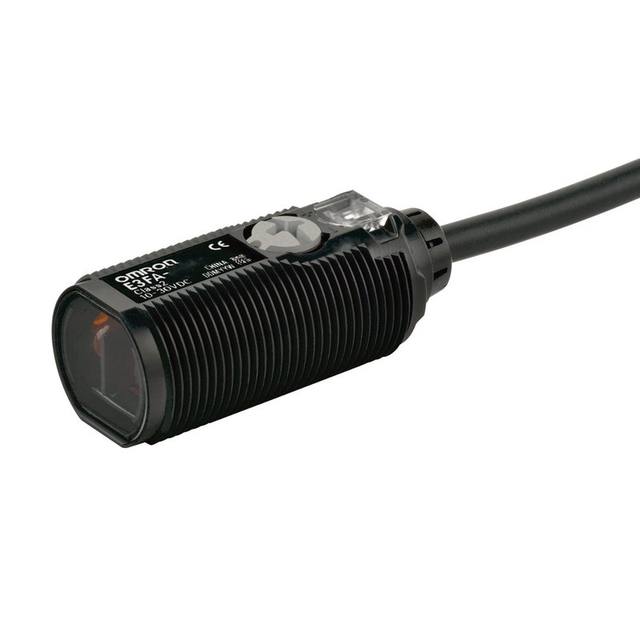
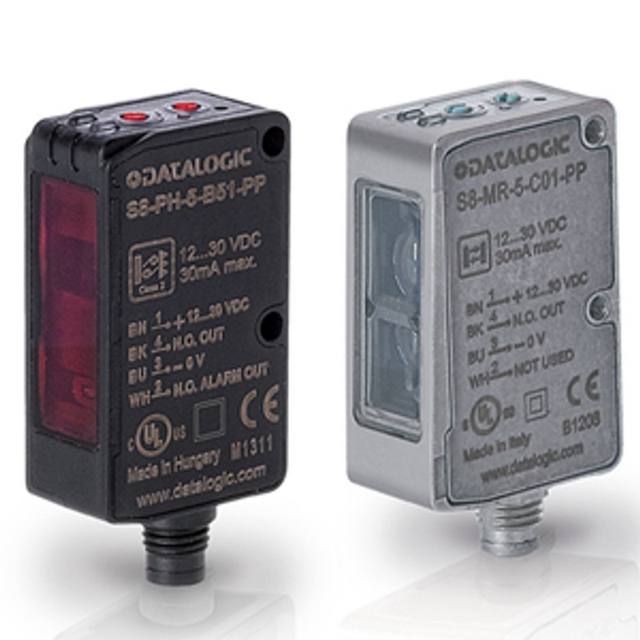
The E3Z-D61 is a compact diffuse-reflective photoelectric sensor with a built-in amplifier and a 5-100 mm sensing distance. It uses an LED light source, provides an NPN output with Light-ON/Dark-ON selection, a response time of 1 ms max, and runs on 12-24 VDC. The housing is rated IP67 (IEC) and is supplied pre-wired with a 2 m cable.
The Omron E3Z-D61 is a compact diffuse-reflective photoelectric sensor with a built-in amplifier, meaning the emitter, receiver and signal-conditioning electronics all live in one self-contained housing rather than in a separate amplifier block. In diffuse mode the emitter and receiver sit together in that single housing: its 660 nm red LED projects a visible spot at the target, and detection relies on light scattered back from the object's own surface rather than from a dedicated reflector or an opposed receiver. That makes installation single-sided, which is its main practical advantage, but it also means the effective range is target-dependent. The published 5-100 mm sensing distance assumes a cooperative, reasonably diffuse target; dark, glossy, transparent or steeply angled surfaces return less light and shorten the usable distance, so the spot should be aimed at the most consistently reflective face of the part. The visible red beam helps here because you can see where it lands and position it by eye during commissioning.
Electrically the sensor runs on 12-24 VDC and provides an NPN switching output, so it sinks current to the load and expects to be wired against a positive common, which is the convention to confirm against the PLC or vision controller input card before connecting. Light-ON / Dark-ON selection lets you choose whether the output asserts when the target is present (light returned) or when it is absent, so the same device can act as a part-present confirmation or a gap/clearance detector without rewiring. With a response time of 1 ms maximum for operate or reset, it can resolve objects passing at conveyor and indexing speeds and switch a corresponding stream of pulses, which is what matters when the sensor is used as a presence detector rather than a precision-timed event source.
In a vision context the E3Z-D61 is best understood as a position and presence device rather than an imaging or trigger-grade timing component. Its natural role is to detect that a part has arrived at an inspection station, gate the start of an acquisition sequence, count items, or confirm a feature is present before or after the camera does the measurement. The NPN output drives a PLC or vision-controller digital input that in turn issues the camera trigger and any strobe; the sensor itself carries no camera, optics or illumination control. The housing is PBT and rated IP67 to IEC, and the device is rated for -25 to 55 degC operation, so it tolerates dusty and wet packaging and logistics environments, and it ships pre-wired with a fixed 2 m cable, which fixes the cable length and means routing and any extension must be planned at design time.
Best for
Part-present confirmation on a packaging line, detecting that a carton, tray or product is at the fill or seal station before the camera inspects it
Gating image acquisition in a packaging-inspection cell by signalling part arrival to the vision controller, which then issues the camera trigger and strobe
Counting and presence detection of boxes or parcels in logistics sortation, where single-sided diffuse mode avoids mounting a reflector across the conveyor
Gap and clearance detection between items on an indexing conveyor using Dark-ON output to flag missing or mis-fed parts
Detecting product presence in food and beverage handling areas where the IP67 PBT housing tolerates moisture and dust
Selection notes
Confirm the target's reflectivity and the actual standoff: the 5-100 mm range applies to cooperative diffuse surfaces, so dark, shiny, transparent or angled parts reduce usable distance and may need the spot aimed at a more reflective face or a different sensing method entirely.
Verify the input wiring is compatible with a sinking NPN output and a 12-24 VDC supply; if the PLC or vision controller input card expects a sourcing PNP signal, this variant will not interface directly and a PNP version or an interposing relay is needed.
Treat it as an arrival or presence signal feeding a vision controller's trigger logic, not as a precision strobe timing source; the 1 ms response governs how fast parts can be resolved, while the camera and lighting controller handle exposure timing.
Plan for the fixed 2 m pre-wired cable: there is no connector to swap, so cable routing, strain relief and any required extension must be designed in, and the device cannot be quickly field-replaced by unplugging.
Use the Light-ON / Dark-ON selection to match the detection intent (part-present versus gap/missing-part) before considering alternative sensors, and confirm the -25 to 55 degC and IP67 ratings cover the installation's temperature and moisture exposure.
Specifications: General
Brand
Omron / Sentech
Sensor type
Photoelectric (diffuse-reflective)
Specifications: Performance
Range / distance
5-100 mm
Response time
1 ms max (operate or reset)
Specifications: Interface
Connection
Cable
Specifications: Electrical
Supply voltage
12-24 VDC
Specifications: Environment
IP rating
IP67 (IEC)
Operating temperature
-25 to 55 degC
Specifications: Mechanical
Housing material
PBT
Specifications: Sensing
Sensing method
Diffuse
Light source
Red LED, 660 nm
Specifications: Output
Output type
NPN
Applications this camera is commonly selected for. Open one to see the full recommended hardware and approach.
These steps take an Omron Sentech (STC) camera from the box to a stable first image and on to your own application. They apply across the GigE Vision, USB3 Vision and CoaXPress STC families; the interface only changes how you cable and power the camera.
Download and install the Sentech SDK on the host PC. The package provides StViewer, the viewing and configuration software you use to bring the camera up, and StApi, the programming SDK you integrate later. Because the cameras are GenICam/GenTL-compliant, StApi also registers a GenTL producer, so any GenICam-compliant third-party vision software can discover and drive the camera as an alternative front end.
2. Cable, power and connect the camera
Connect according to the interface. GigE Vision: link to a Gigabit NIC (use PoE or the separate power input) and put the camera and host on the same subnet; for USB3 Vision use a USB 3.x port and a certified cable; for CoaXPress (STC) connect to a CoaXPress frame grabber, which also supplies Power-over-Coax. Then open StViewer and let it enumerate the camera. If a GigE camera does not appear, check the IP configuration and firewall, and on USB3 confirm the host bandwidth and driver.
3. Configure exposure, gain and white balance
Open the device in StViewer and start a live stream. Set exposure and gain for a well-exposed, low-noise image: raise exposure first and only add gain when more light or a faster shutter is not an option, keeping exposure short enough to freeze motion on global-shutter models. On colour cameras, run white balance under your actual production lighting. Adjust the lens aperture and focus on a representative target before tuning anything else.
4. Set the trigger and grab a first image
Start in free-run (continuous) acquisition to confirm a clean, stable image. For inline inspection switch to hardware or software triggering: select the trigger source, set the active edge and any delay, and wire the strobe or illumination to the camera's I/O so lighting fires with each exposure. Acquire and save a frame in StViewer; this saved image is your reference for the SDK stage and for downstream inspection.
5. Move to the StApi SDK (or any GenICam software)
Once the image is stable, reproduce the same settings in code. Use StApi to open the device, apply the GenICam features you validated in StViewer (exposure, gain, trigger, pixel format) and grab frames into your application via the bundled C++, C, C#/.NET or Python interfaces; the included samples are the fastest starting point. Prefer a different stack? The same GenICam/GenTL camera works with third-party vision libraries. With a reliable feed, you can route it into a deep-learning inspection such as Rosepetal for AI-based defect detection.
Frequently asked questions
The E3Z-D61 has a 5-100 mm sensing distance in diffuse-reflective mode. Because diffuse sensing relies on light scattered back from the object's own surface, the usable distance is target-dependent: dark, glossy, transparent or steeply angled surfaces return less light and shorten the effective range, while light, matte surfaces perform near the full distance.
It provides an NPN switching output and runs on 12-24 VDC. As an NPN device it sinks current to the load, so it suits a digital input expecting a sinking signal against a positive common. It is typically wired to a PLC or vision-controller input that then issues the camera trigger; confirm the input card accepts NPN before connecting.
Yes. The sensor offers Light-ON / Dark-ON selection, so you can configure the output to assert when the target returns light (part present) or when light is absent (part missing or a gap), letting the same unit serve as either a presence detector or a gap detector.
Its response time is 1 ms maximum for operate or reset, which is fast enough to resolve parts moving at typical conveyor and indexing speeds and to produce a corresponding switching signal for counting or arrival detection.
The housing is PBT and rated IP67 to IEC, and the sensor is rated for -25 to 55 degC operation, making it suitable for dusty and wet packaging, logistics and food and beverage areas. It is supplied pre-wired with a fixed 2 m cable rather than a plug connector, so plan cable routing accordingly.